Inside Quality Inspection for Bulky Office Supplies
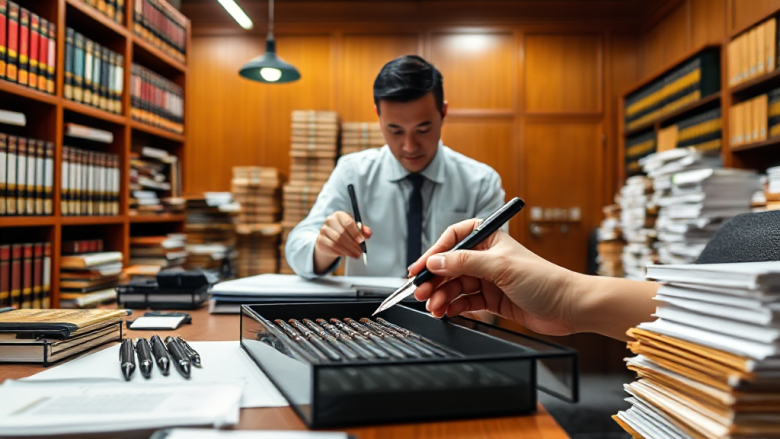
On the inspection table, a tray of retractable pens sits under a daylight lamp. A technician clicks each cap into place, draws a slow line across a test card, then squeezes the barrel between thumb and forefinger to check for flex. Behind her, pallets of boxed bulky office supplies wait for release. Nothing moves to the container until that tray passes. This is the routine that decides whether a shipment leaves the factory or goes back to the line, and for European importers it is often the difference between a smooth retail season and a costly returns problem.
I have spent years on factory floors running pre-shipment inspections for stationery and paper products. What follows is the actual sequence my team follows, from raw material intake to container loading, including the defect categories we record and the pass/fail logic we apply. It is written for importers, wholesalers and corporate buyers who need to understand what a credible inspection report should contain.
Why bulky office supplies need a different inspection rhythm
Bulky office supplies are not a single product. The category covers high-volume, low-unit-value goods that ship in large cartons: ballpoint and gel pens, markers, correction tape, staplers, punches, folders, lever arch files, ring binders, box files, note pads, sticky notes, envelopes, and paper reams. These items are bulky in the logistics sense rather than the fragile sense. They consume container space, they are stacked high, and they are frequently mixed into multi-SKU orders where one weak component can pull down an entire pallet.
That combination changes the inspection rhythm. A single premium item might justify a slow, near-total check. A container of 400,000 pens cannot be inspected that way, so we rely on statistical sampling. At the same time, the goods are dense and heavy, which means carton compression, pallet stability and moisture exposure matter as much as the product itself. An inspection that only opens a few inner boxes and ignores the pallet build is not an inspection; it is a formality.
For importers sourcing through a Hong Kong-based partner, the practical question is not whether an inspection happens, but whether it happens against a written specification. Without a signed golden sample and a measurable checklist, sampling becomes subjective, and subjective sampling produces disputes.
Raw material intake and the golden sample baseline
The inspection timeline actually begins before production, at raw material intake. For a pen order, that means incoming barrels, caps, ink cartridges, springs and clips. For a paper order, it means reels or sheets, board thickness, and the certification documents that accompany them. We verify material against the approved specification sheet and against the retained golden sample signed at order confirmation.
The golden sample is the anchor for everything that follows. It is sealed, dated and stored at the factory, and a duplicate is held by the sourcing office. When a technician later questions whether a clip feels too loose or a folder board feels too thin, the answer is not an opinion. It is a comparison against the sealed reference.
Material intake checks include:
- Ink batch code and viscosity confirmation for writing instruments
- Plastic resin grade and colour match against the approved master
- Board thickness and grammage measurement for files and folders
- Paper certification marks and chain-of-custody paperwork for fibre-based goods
- Metal component hardness spot checks for staplers and punches
This is also where sustainability claims are validated. If a buyer has specified certified fibre or recycled content, we confirm the documentation at intake rather than at shipment, because by then the material is already inside the product. For buyers building a programme around sustainable Office Supplies, catching a documentation gap at intake is far cheaper than catching it at the port.
In-line checks on the production line
Between intake and final packing, we run in-line checks at defined intervals. These are not full inspections. They are rapid, repeatable tests that catch drift before a whole shift of output is affected.
For writing instruments, the in-line routine is tactile and mechanical. A technician takes a fixed number of units per hour and tests ink flow by drawing a continuous line of specified length, checking for skipping, blotting and inconsistent line weight. Cap fit is tested by click-on and pull-off force, because a cap that releases too easily will leak in transit and a cap that grips too tightly will crack. Barrel strength is tested by flexing and by drop testing from a set height onto a hard surface.
For filing and paper products, the in-line focus shifts to dimensional accuracy and function. Lever arch mechanisms are opened and closed repeatedly to check spring tension and alignment. Ring binders are checked for ring gap, because a gap of even a fraction of a millimetre causes paper to tear. Folder scores are checked for clean folding without cracking. Note pads are checked for sheet count, glue strength and edge trim.
Print quality is checked throughout. Logos, barcodes and regulatory text must be legible and correctly positioned. For buyers running private label office products, this is where brand risk concentrates. A misregistered logo or a wrong barcode is not a cosmetic issue; it can trigger retail chargebacks and re-labelling costs in Europe.
Every in-line finding is logged with time, line, machine and operator. When a defect trend appears, production pauses for adjustment rather than continuing to build inventory that will later be rejected.
AQL sampling, defect classes and pass/fail logic
The core of pre-shipment inspection is acceptance sampling under AQL, the Acceptable Quality Limit. Rather than inspecting every unit, we draw a statistically valid sample from the finished, packed lot and judge it against defined defect classes.
Defect classes are agreed in advance and written into the inspection protocol:
- Critical defects: safety hazards, sharp edges, broken components, contamination, or anything that could injure an end user. Zero tolerance.
- Major defects: functional failures that make the product unusable or unsellable, such as a pen that does not write, a binder that will not close, or a wrong printed logo.
- Minor defects: cosmetic or minor issues that do not affect function, such as light scuffing, slight colour variation within tolerance, or minor print speckling.
Sample sizes and acceptance numbers are set according to the agreed AQL levels, typically stricter for majors and criticals and looser for minors. The logic is straightforward. Any critical defect fails the lot. If the number of major defects in the sample exceeds the acceptance number, the lot fails. Minor defects are tolerated up to a higher threshold because rejecting a container over light scuffing is not commercially rational.
Critically, the sample must be drawn from packed cartons, not from the end of the line. Inspecting unpacked goods tells you what the line can produce. Inspecting packed goods tells you what the customer will receive.
Where a buyer is running white label office products across multiple retail chains, we also verify that the correct packaging variant, language panel and article number are on the correct pallet. Mixed packaging is one of the most common and most avoidable causes of European warehouse rejection.
Carton, pallet and container loading verification
Product quality alone does not guarantee a clean delivery. Bulky office supplies are heavy and stack high, so packaging and loading verification is a distinct stage.
We check carton board grade, glue lines, tape coverage and print accuracy. We measure carton dimensions against specification, because a carton that is even slightly oversized reduces the number of units per pallet and can break a container plan. We verify quantity per carton by counting a sample of sealed cartons.
Pallet checks cover stacking pattern, interlocking, corner protection, stretch wrap tension and labelling. For sea freight to Europe, moisture control matters, so we confirm desiccant placement and liner bags where specified. A pallet that shifts in transit arrives with crushed corners and torn cartons, which is a claims problem regardless of how good the pens are.
Before loading, we confirm container condition: no holes, no rust streaks, no residual odour from a previous cargo, and a valid inspection record. During loading, we monitor the stow plan, weight distribution and bracing. Photographs are taken at each stage, from empty container to sealed doors with the seal number visible.
The final report combines product inspection results, packaging verification, loading evidence and a clear pass, fail or conditional release decision. If the lot fails, the report identifies the defect class and the corrective action required, and re-inspection is scheduled after rework.
What importers should ask for before booking freight
A quality inspection is only as strong as the specification behind it. Before confirming a bulky office supplies order, importers should ensure that a golden sample is sealed and retained, that AQL levels and defect definitions are agreed in writing, and that the inspection covers packed goods, packaging and loading rather than product alone.
Ask for the inspection report with dated photographs, sample sizes, defect counts and the acceptance numbers used. Ask who performed the inspection and whether they are independent of the production line. Ask what happens if the lot fails, and who bears the cost of rework and re-inspection.
On the factory floor, the inspection table is where promises become measurable. Ink flow, cap fit, barrel strength, ring gap, board thickness, carton dimensions and seal numbers are not abstractions. They are the specific points where a shipment either earns its release or returns to the line. Importers who build their sourcing around that discipline get fewer surprises at the port, cleaner retail launches, and a supply chain that can be defended with documents rather than assurances.